How to Reduce Screen Plugging When Screening Sticky Materials

Screen plugging—commonly called blinding—is one of the most persistent challenges in processing sticky, moist, or clay‑laden materials. When fine particles adhere to the mesh openings, throughput drops, separation efficiency plummets, and downtime for manual cleaning becomes a costly routine. Whether you are screening wet sand, fertilizer, coal fines, or recycled aggregates, understanding how to prevent blockages is essential to maintaining a profitable operation. With decades of field experience, Haiside has developed a systematic approach that combines machine design, media selection, and daily practices to keep your screens running clean. This article explores the root causes of plugging and delivers actionable solutions you can apply immediately.

Understanding the Root Causes of Screen Plugging in Sticky Materials

Before you can fix screen blinding, you need to understand why it happens. Sticky materials contain moisture, clay, or organic binders that create a thin film on both the particle surface and the screen wire. When these particles pass through the mesh, three mechanisms dominate:

  • Adhesion: Liquid bridging causes particles to cling to the wire, especially near the aperture edges.
  • Cohesion: Particles agglomerate and form a cake that blocks entire sections of the screen.
  • Mechanical wedging: Near‑size particles become lodged in openings, and the sticky coating prevents them from being ejected by vibration.

The severity depends on material moisture content, clay percentage, particle shape, and ambient humidity. High‑frequency, low‑amplitude vibration typical of many screens can actually worsen plugging by compacting particles into the mesh. A thorough understanding of your material’s rheology is the first step toward choosing the right countermeasure.

Key Design Features to Minimize Screen Blockage
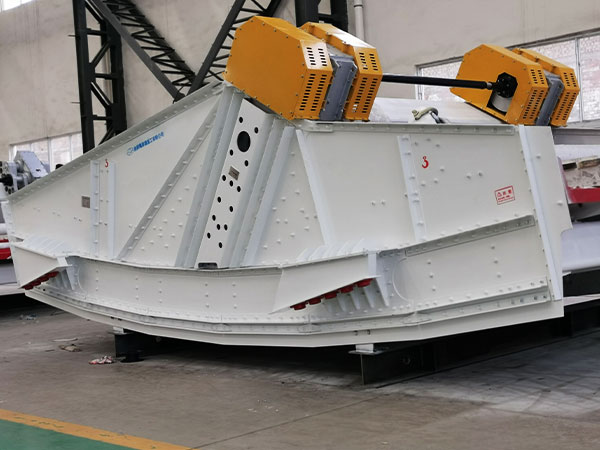
Not all screening equipment is built to handle sticky feeds. Haiside engineers specify several design modifications that dramatically reduce plugging:

Screen Tension and Material Selection

Loose screen panels vibrate with a different frequency than the deck, allowing material to settle into pockets. Proper tensioning—using a pneumatic or hydraulic tensioning system—ensures the mesh remains taut, reducing the opportunity for particles to stick. For the media itself, polyurethane and rubber panels with self‑relieving hole shapes (e.g., slot‑ or diamond‑shape openings) shed sticky fines far better than woven wire cloth. Haiside recommends a minimum opening size of 1.2 times the largest particle dimension to reduce wedging.

Self‑Cleaning Mechanisms

Ball decks and ultrasonic transducers are proven add‑ons. Ball decks place resilient rubber balls beneath the screen; the natural vibration causes them to bounce against the underside of the mesh, dislodging stuck particles. For ultra‑fine openings (down to 45 microns), ultrasonic vibration of the screen wire breaks the surface tension that holds fines to the wire. In field trials cited by Haiside, ultrasonic systems reduced plugging by 70–90% in silica flour and cement applications.

Heated Screens or Anti‑Stick Coatings

Applying mild heat (40–60 °C) to the screen surface evaporates surface moisture, disrupting adhesion. Electric resistance heating elements embedded in the deck or spray‑on PTFE‑based coatings are common approaches. For heavily clay‑contaminated materials, Haiside uses a hybrid solution: a heated screen combined with a wetting agent spray that reduces surface tension. This combination is particularly effective in the aggregate and mining sectors.

Operational Best Practices for Reducing Plugging

Even the best‑designed screen will blind if operated incorrectly. The following practices have been refined over hundreds of installations by Haiside service teams:

Adjusting Feed Rate and Angle

Overfeeding is the most common operational mistake. When material builds up on the deck, the weight of the bed presses sticky fines into the openings. Maintain a bed depth no greater than three times the opening size. If your screen has an adjustable incline, increasing the angle to 25–30° for sticky materials accelerates material travel, reducing contact time and giving particles less chance to adhere. However, too steep an angle can cause oversize particles to bounce and degrade. Haiside recommends a step‑wise adjustment while monitoring undersize recovery.

Regular Cleaning Protocols

Despite preventive measures, some plugging is unavoidable. The key is to intervene before blinding becomes severe. A simple checklist includes:

  • Spray bars with high‑pressure water (if material can tolerate moisture) to wash the mesh between shifts.
  • Air knives or compressed air lances to blow out lodged near‑size particles.
  • Mechanical scrapers—non‑metallic to avoid damaging the screen—that sweep the underside of the deck while it runs.

For screens handling very sticky materials like wet fly ash or bio‑sludge, Haiside recommends scheduling a 5‑minute manual inspection every two operating hours during the first week of operation, then adjusting the frequency based on observed plugging rate.

Troubleshooting Common Plugging Scenarios
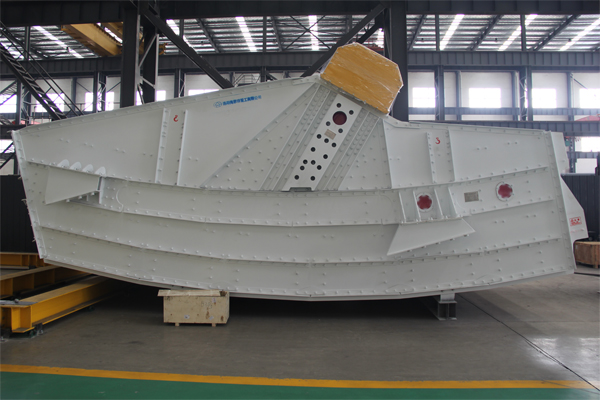
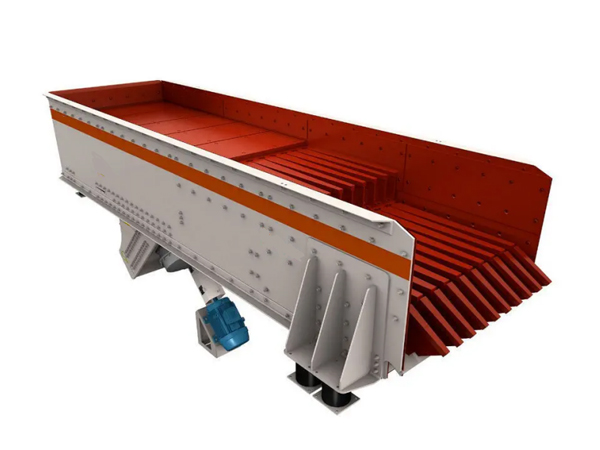
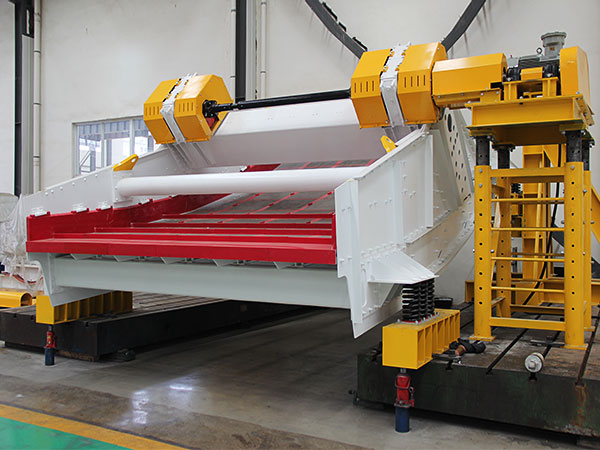
Double banana sieve

Even with the best practices, you may still encounter specific problems. Here are three common situations and how Haiside experts address them:

  • Persistent plugging in the top‑deck only → Likely a feed distribution issue. Check for a skewed feed box or a grizzly that is allowing oversized lumps to hit the screen. Install a feed distributor to spread material evenly.
  • Blinding that worsens during humid weather → Condensation on the screen wire increases adhesion. Evaluate whether a heated screen or a dehumidifier in the screening enclosure is justified for seasonal conditions.
  • Plugging concentrated in the center of the screen → Usually indicates a worn or sagging screen panel. Replace the panel and re‑tension. Haiside’s modular polyurethane panels with reinforced center support eliminate this failure mode.

Summary: A Multi‑Layered Approach to Tackle Sticky Screening

Reducing screen plugging requires more than a single fix—it demands an integrated strategy that addresses material behavior, machine design, and daily operation. Start by characterizing your feed: moisture content, clay percentage, and particle size distribution. Then select a screening solution that incorporates proper tensioning, self‑cleaning aids, and potentially heated surfaces. On the operational side, control feed rate, adjust incline, and implement a disciplined cleaning schedule.

Haiside has engineered screening systems for hundreds of sticky material applications across mining, recycling, chemical, and food processing industries. Our application engineers can analyze your specific plugging issue and recommend retrofits or new equipment that will reduce downtime by up to 60% and increase throughput by 15–25%. Contact us to discuss your screening challenge—we’ll help you keep your mesh clear and your production flowing.
Mobile Vibrating Screens for Construction and Demolition Recycling

In construction and demolition (C&D) recycling operations, the ability to efficiently separate and sort mixed debris into usable aggregates is critical for both profitability and environmental compliance. Mobile vibrating screens have emerged as essential equipment on job sites where traditional fixed screening plants are impractical. These self-contained units offer flexibility, rapid deployment, and high throughput—making them indispensable for contractors and recyclers who need to process varying volumes of material at different locations. Understanding the technical parameters and operational benefits of mobile vibrating screens is the first step toward selecting the right solution for your recycling operation.

Why Mobile Vibrating Screens Are Essential for C&D Recycling

C&D waste typically contains concrete, asphalt, wood, metals, plastics, and soil—materials that require precise classification to recover value. Mobile vibrating screens are designed to handle this heterogeneous feed with minimal setup time. Unlike stationary systems, mobile units can be moved directly to the demolition site or stockpile, reducing transportation costs and eliminating the need for permanent infrastructure. Their ability to perform primary, secondary, or even tertiary screening in a single pass makes them versatile tools for producing multiple product fractions such as 0–5mm fines, 5–20mm aggregates, and oversized rejects.

Key Performance Factors in Mobile Vibrating Screens

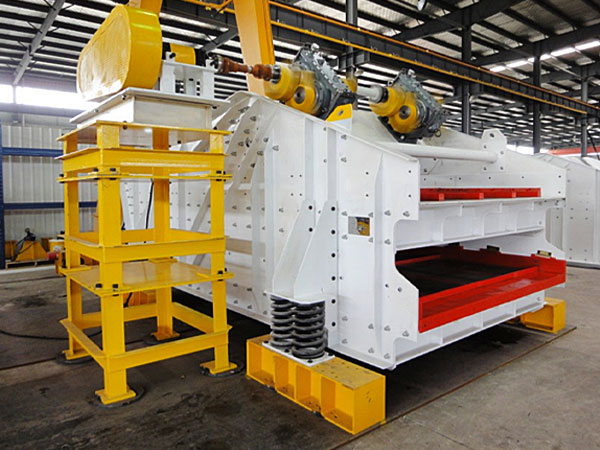
Linear Vibrating Screen

Vibration Mechanism and Stroke

The screening efficiency depends heavily on the vibration pattern—linear or circular motion. For sticky or wet C&D materials, circular motion with adjustable amplitude helps avoid blinding. Mobile screens from Haiside utilize a robust eccentric shaft design that delivers consistent stroke under heavy loads.

Deck Configuration and Surface Area

A larger screening area directly correlates to higher throughput. Standard mobile units offer double- or triple-deck configurations. Operators must balance the desired number of fractions against the machine’s overall transport dimensions. Haiside models incorporate quick-change screen panels to reduce downtime when switching between applications.

Mobility and Setup Efficiency

Time is money on active demolition sites. Hydraulic folding hoppers, track-mounted chassis, and wireless remote controls allow one operator to set up the plant in minutes. Many Haiside mobile screens feature a durable crawler undercarriage with high ground clearance for navigating rough terrain.

Advantages of Haiside Mobile Vibrating Screens Over Conventional Models

Haiside has engineered its mobile screening range with feedback from hundreds of recycling professionals. The following advantages set them apart:

  • High-frequency vibrating mechanism that prevents pegging and clogging even with moist demolition debris.
  • Integrated overband magnet available as a factory option to remove ferrous metals before screening.
  • Intelligent control system that monitors belt speed, vibration frequency, and engine load, adjusting parameters automatically for consistent quality.
  • Modular design allowing the main screenbox to be swapped between different sized decks in under two hours.
  • Compliance with European Stage V and EPA Tier 4 final emission standards, making them suitable for both urban and remote sites.

Selecting the Right Mobile Vibrating Screen for Your Application

Every recycling operation has unique constraints. Consider these criteria before making a purchase decision:

  1. Feed size and abrasiveness: Larger feed requires a heavy-duty feed hopper and reinforced screen box. Haiside offers wear-resistant liners as an upgrade.
  2. Required output fractions: If you need three clean products, a triple-deck unit with adjustable angle is ideal.
  3. Site accessibility: Tracked vs. wheeled mobility—tracks offer superior traction on loose aggregate.
  4. Power source: Diesel-hydraulic versus electric. For sites with grid connection, electric models reduce noise and emissions.
  5. After-sales support: Haiside provides genuine spare parts and on-site training within 48 hours for major regions.

Frequently Asked Questions

Can a mobile vibrating screen handle concrete rebar?

Yes, but only after primary crushing. Mobile screens are designed for sized feed. Reinforce concrete must first go through a jaw or impact crusher. Haiside screens can then separate the crushed concrete from any remaining steel fragments.

How often should screen media be replaced?

Depends on material abrasiveness and operating hours. Typically, polyurethane panels last 3–6 months in C&D applications. Haiside recommends monthly inspections and immediate replacement if any tear exceeds 20 mm.

What is the typical fuel consumption of a mobile vibrating screen?

A mid-sized diesel unit (e.g., Haiside HS-1540) consumes approximately 18–25 liters per hour under normal load. Electric-driven models consume 30–40 kW/h.

Conclusion

Cooperation Customer

Mobile vibrating screens are a strategic investment for any C&D recycling operation aiming to improve material recovery rates while maintaining site flexibility. By focusing on vibration performance, deck configuration, and mobility features—and by partnering with a reliable manufacturer like Haiside—recyclers can achieve consistent product quality and lower total cost of ownership. Evaluate your specific material characteristics and site requirements, then choose a model that aligns with your long-term operational goals.

Comparing Metal and Polyurethane Screens for Vibrating Equipment

Selecting the right screen media for vibrating equipment is a critical decision that directly impacts processing efficiency, product quality, and operating costs. Two of the most widely used materials—metal and polyurethane—offer distinctly different characteristics, and choosing between them requires a clear understanding of their performance under real-world conditions. This article provides an objective, technical comparison of metal and polyurethane screens, covering wear life, screening accuracy, operational considerations, and total cost of ownership. For operations seeking reliable, application-matched solutions, Haiside supplies both types of screen panels, enabling customers to make data-informed choices based on their specific material properties and production goals.

Overview of Metal Screens and Polyurethane Screens

Metal Screens: Construction and Typical Applications

Metal screens are manufactured from woven wire cloth or perforated metal plates. Common materials include high-carbon steel, stainless steel, and spring steel. Their open structure provides a high percentage of open area (typically 40–60%), which facilitates high throughput and efficient fines removal. Metal screens are widely used in mining, quarrying, and aggregate processing for coarse to medium screening where impact resistance and rapid material movement are priorities. However, they are susceptible to abrasion, corrosion in wet environments, and fatigue failure under heavy loads.

Polyurethane Screens: Composition and Key Characteristics

Polyurethane screens are made from cast or molded polyurethane elastomers, often reinforced with steel inserts for structural integrity. They offer superior resistance to abrasion and corrosion compared to metal, and their flexible nature reduces blinding and pegging in sticky or moist materials. The open area is lower (typically 30–45%) due to thicker cross-sections, but the material’s wear life can be 3 to 5 times longer than metal in abrasive conditions. Polyurethane panels are quieter in operation and lighter in weight, reducing dynamic loads on the vibrating equipment.

Key Performance Comparison

When evaluating these two screen types, several performance parameters must be weighed against each other. The following list highlights the most critical differences:

  • Wear Resistance: Polyurethane generally outlasts metal by a factor of 3–5 in abrasive applications. Metal screens wear more quickly, especially at wire intersections and along perforation edges.
  • Screening Efficiency: Metal screens typically offer higher open area, leading to greater throughput. Polyurethane’s flexibility can actually improve stratification and reduce near-size particle retention, but reduced open area may lower capacity.
  • Blinding and Peeling: Polyurethane is less prone to blinding because of its non-stick surface and ability to flex. Metal screens tend to clog with moist or clay-rich materials.
  • Noise and Vibration: Polyurethane dampens noise by 5–10 dB compared to metal, creating a quieter working environment. It also transmits less vibration to the support structure.
  • Weight: Polyurethane panels are significantly lighter, reducing startup torque and wear on bearings and frames.
  • Temperature Tolerance: Metal screens can withstand temperatures up to 400°C (depending on alloy), while polyurethane is typically limited to 80–90°C.

Long-Term Cost Analysis (Total Cost of Ownership)

Initial purchase price often favors metal screens, which can be 30–60% less expensive per panel than equivalent polyurethane. However, total cost of ownership (TCO) must account for replacement frequency, downtime losses, and maintenance labor. In high-abrasion environments (e.g., iron ore, copper, crushed granite), a single polyurethane panel may replace three to five metal panels over its life. Reduced changeover downtime and lower inventory requirements can further tilt the balance. For wet screening operations where corrosion accelerates metal degradation, polyurethane offers even greater economic advantage. Haiside provides detailed TCO estimates to help operators compare scenarios specific to their throughput and material characteristics.

Application-Specific Recommendations

Choosing between metal and polyurethane is largely dictated by the material being processed and the operating conditions. Below are general guidelines:

  • High-Impact Coarse Screening: Metal screens (especially perforated plate) are preferred for top-deck scalping where large rocks cause repeated impact. Polyurethane may deform or tear under such loads.
  • Fine and Medium Screening in Abrasive Ores: Polyurethane screens are ideal for high-wear, fine particle applications. Their long life reduces maintenance frequencies.
  • Wet Screening or Dewatering: Polyurethane outperforms metal due to corrosion resistance and reduced blinding. Polyurethane slotted panels are common in dewatering applications.
  • Heavy-Duty Dry Screening with High Tonnage: Metal screens with large open area maximize capacity, but allow for more frequent replacements.
  • Noise-Sensitive Environments: Polyurethane is the better choice when regulatory or workplace noise limits must be met.

Operators with varying material types may benefit from using both technologies on different decks within the same machine—a common practice recommended by Haiside engineers.

Conclusion: Making the Informed Decision

The choice between metal and polyurethane screens for vibrating equipment is not a one-size-fits-all proposition. Metal screens offer higher open area and lower upfront cost, making them suitable for impact-heavy coarse applications. Polyurethane screens deliver extended wear life, reduced blinding, and quieter operation, yielding lower TCO in abrasive, wet, or fine-screening environments. By analyzing throughput requirements, material abrasiveness, moisture content, and replacement logistics, operators can select the optimal screen media. Haiside supports this decision with a full portfolio of both metal and polyurethane screen panels, backed by decades of field experience. To evaluate which option fits your process, consult with Haiside screening specialists who can provide application-specific recommendations and life-cycle cost comparisons.

Measurable Benefits of Proper Vibrating Screen Tensioning

Proper tensioning of vibrating screen mesh is often underestimated in its impact on overall screening performance. Yet, for operations handling bulk materials—from aggregate to minerals—the tension applied to the screen cloth directly determines throughput accuracy, wear life, and operating costs. When tension is too loose, the screen flexes excessively, leading to premature fatigue, blinding, and inefficient particle separation. When over-tightened, the mesh may crack or distort, reducing screening area. In either case, measurable losses occur. This article examines the quantitative advantages of maintaining correct screen tension, drawing on field data and engineering principles, and explains how Haiside tensioning systems help operators achieve consistent, verifiable results.

1. The Direct Impact on Screening Efficiency and Throughput

The primary function of a vibrating screen is to separate particles by size. Screen tension plays a critical role in how effectively the mesh transmits vibration to the material bed. A properly tensioned screen maintains a uniform amplitude across its surface, ensuring that each particle receives the same acceleration and stratification force.

Quantifying Particle Separation Accuracy

Studies have shown that a tension deviation of just 10% from optimal can reduce screening efficiency by 15–20%. Loose screens allow the mesh to flutter independently of the screen deck, creating localized areas of reduced vibration. Oversized particles may pass through momentarily stretched openings, while near-size particles become trapped, increasing pegging. Conversely, a properly tensioned screen from Haiside maintains consistent opening dimensions, resulting in tighter cut-point control. In a typical 2-deck operation, proper tension can improve oversize recovery by 8–12% and reduce misplaced fines in oversize product.

How Tension Affects Material Flow Rate

Throughput is directly linked to the open area available for material passage. When a screen is loose, it bows under the load, reducing the effective screening surface. Over multiple cycles, this bowing increases, further restricting flow. Proper tensioning ensures the mesh remains flat and taut, maximizing open area. Field measurements indicate that restoring correct tension can increase mass flow by 6–10% on the same screen deck without changing stroke or speed. For a plant processing 500 tons per hour, this translates to an additional 30–50 tons per hour of correctly sized product.

2. Extended Screen Life – Reducing Replacement Frequency

Cooperation Customer

Screen cloth is a consumable with significant cost implications. Many operators accept a short life as normal, but the failure mode is often linked to improper tension rather than inherent wear. A screen that is too loose undergoes repeated flexing at the tensioning hooks and around the support bars. This cyclic bending stress causes fatigue cracks that propagate quickly, leading to sudden failure.

Stress Distribution and Fatigue Prevention

When a screen is correctly tensioned, the tensile stress is evenly distributed across the entire cloth. The vibration energy is transmitted uniformly, and the screen’s natural frequency remains stable. Industry data shows that proper tension can extend screen life by 30–50% compared to loose operation. In one documented case from a quarry using Haiside tensioning rails, the average screen life increased from 4 weeks to 6.5 weeks, a 62% improvement, solely by implementing a tensioning procedure with a tension gauge.

Case Data: Proper vs. Improper Tensioning

  • Improper (loose): Fatigue failure at hook ends within 2–3 weeks; frequent blinding requiring manual cleaning; replacement cost $1,200 per deck per month.
  • Proper tension (Haiside calibrated): Wear-out failure (abrasive wear) after 6–8 weeks; no blinding-related downtime; replacement cost $600 per deck per month.

The cost reduction per deck exceeds 50% when factoring in labor for tension adjustments and cleaning. Additionally, proper tension reduces the risk of sudden mesh collapse, which can damage screen decks and cause hazardous debris ejection.

3. Lower Operating Costs Through Reduced Downtime and Maintenance

Unscheduled downtime costs far more than the value of lost production. Screen blinding, plugging, or breakage forces the entire line to stop. Correct tensioning minimizes these events, directly improving plant availability.

Energy Consumption Considerations

Loose screens absorb more energy from the vibrator because the mesh’s motion is out of phase with the deck. The motor must work harder to maintain stroke. Energy monitoring studies indicate that properly tensioned screens reduce power draw by 5–8% compared to loose conditions. Over a year, this represents thousands of dollars in savings for a typical 200 kW screen drive.

The Cost of Untensioned Screens

Operators who skip tensioning checks often face compound costs: accelerated wear of support frames, tighter screen bolts, and increased wear on rubber buffers. A common hidden cost is the need to replace screen cloth more frequently, which not only adds material expense but also requires maintenance labor and reduced throughput during changeover. By adopting a systematic tensioning process with Haiside’s tensioning indicators, a mid-size aggregate plant reported reducing screen-related downtime by 40% and lowering annual screen cloth expenditure by $18,000.

4. Why Haiside Tensioning Solutions Deliver Consistent Results

High Frequency Dehydration Vibrating Screen

Haiside has engineered tensioning systems that address the root causes of poor tension control. Unlike generic bolt-down methods, Haiside products provide repeatable tension with visual or mechanical indicators, eliminating guesswork.

  • Precision tension adjustment: Haiside tension rails and cam systems allow for uniform clamping force across the entire width of the screen, preventing localized slack.
  • Durable construction: Made from abrasion-resistant steel with corrosion-resistant coatings, Haiside components withstand harsh screening environments without losing grip.
  • Fast installation: Integrated tension indicators enable operators to achieve correct tension in minutes, not hours.
  • Technical support: Haiside provides on-site tensioning audits and recommended tension values based on screen type, aperture, and material conditions.

For operations seeking to verify the benefits discussed above, Haiside offers a simple call-to-action: request a tensioning performance analysis. By comparing current screen performance against a benchmark with Haiside equipment, operators can directly measure improvements in efficiency, life, and cost.

Conclusion: Turning Tension into a Measurable Asset

Proper vibrating screen tensioning is not a trivial adjustment—it is a measurable lever for improving plant profitability. The data is clear: correct tension leads to higher screening efficiency, longer screen life, lower energy consumption, and reduced maintenance costs. For operators willing to invest in a systematic tensioning program and quality components like those from Haiside, the return is both immediate and sustained. The next time a screen deck produces off-spec material or fails prematurely, examine the tension first; it may be the simplest fix with the biggest impact.

Avoiding Structural Failures in Heavy-Duty Vibrating Screens

Heavy-duty vibrating screens are the backbone of material processing in mining, aggregates, and industrial sectors. Yet structural failures—cracks in side plates, broken beams, or weld fatigue—remain costly and dangerous. These failures not only halt production but also risk worker safety and escalate maintenance budgets. Understanding why these failures occur and how to prevent them is critical for any operation that depends on consistent screening performance. This article examines the root causes of structural breakdowns and presents proven engineering strategies, including the advanced approaches adopted by leading manufacturers like Haiside, to ensure long-term reliability.

Understanding Structural Failures in Heavy-Duty Vibrating Screens

Structural failures typically manifest in three forms: fatigue cracking, resonance-induced damage, and material degradation. Fatigue cracking, the most common, develops over millions of cycles due to cyclic stress concentrations at weld joints, bolt holes, or geometric transitions. Resonance occurs when the operating frequency aligns with a natural frequency of the structure, amplifying vibration amplitudes beyond design limits. Material degradation can result from corrosion, abrasion, or substandard steel grades that lack sufficient impact toughness.

Root Causes Explained

  • Improper design margins: Many failures stem from inadequate safety factors in the structural frame, particularly at the support beams and cross members.
  • Poor weld quality: Incomplete penetration, slag inclusions, or lack of preheating in thick sections create crack initiation sites.
  • Overlooking dynamic loads: Static calculations miss the amplified forces from eccentric masses and material impacts—real loads can exceed static estimates by 3–5 times.
  • Environmental factors: Moisture, chemical exposure, and temperature extremes accelerate fatigue crack growth.

Key Design Strategies to Prevent Structural Failures

Preventing failures starts at the design stage with a focus on fatigue life optimization. Finite element analysis (FEA) is now standard to simulate stress distribution under dynamic loading. Critical areas such as the discharge end, feed box, and side plate transitions must be reinforced. Haiside engineers, for example, use FEA to identify high-stress zones and apply generous radii, tapered transitions, and ribbed stiffeners to reduce stress concentration factors.

Natural Frequency Avoidance

Every vibrating screen has a range of natural frequencies. Designers must ensure that the operating frequency (typically 800–1200 RPM for heavy-duty screens) is separated from any structural natural frequency by at least 20%. Haiside performs modal analysis on every custom screen model to verify this separation, preventing resonance that can cause rapid failure.

Material Selection and Welding Protocols

High-strength low-alloy (HSLA) steel, such as S690QL or equivalent, is preferred for side plates and cross beams due to its high yield strength and excellent weldability. Welding procedures must strictly adhere to standards like AWS D1.1 with preheating and post-weld heat treatment for thicker sections. Haiside uses robotic welding with real-time monitoring to ensure consistent penetration and minimal heat-affected zone defects.

The Role of Precision Manufacturing and Quality Control

Even the best design fails without manufacturing precision. Flatness tolerances on side plates must be within ±1 mm over 3 meters to prevent asymmetric stress distribution. Bolt holes must be drilled with jigs to avoid misalignment that creates point loads. Haiside’s production line includes CNC plasma cutting, stress-relieving after welding, and 100% ultrasonic testing on all load-bearing welds.

Assembly and Dynamic Balancing

Improper assembly of the exciter unit or uneven distribution of material on screen decks can cause unbalanced forces that accelerate bearing wear and structural fatigue. Haiside employs dynamic balancing within G2.5 grade for all rotating assemblies, and every screen undergoes a 72-hour no-load test run to verify vibration patterns before shipment.

Haiside’s Proven Approach to Structural Integrity

With over a decade of experience in heavy-duty screening solutions, Haiside has developed a comprehensive system that minimizes failure risks. Below are key differentiators compared to conventional designs:

  • Reinforced side plate design: Haiside uses thicker side plates (8–16 mm depending on model) with integrated doubler plates at stress-concentrated zones, extending fatigue life by up to 40%.
  • Optimized beam geometry: Instead of standard rectangular beams, Haiside employs box-section or I-beam profiles with internal stiffeners that reduce deflection under peak loads.
  • Advanced rubber spring mounts: Isolation efficiency exceeds 90%, reducing transmitted vibration to the support structure and lowering the risk of resonance-related failures.
  • Witnessed inspection protocol: Customers or third-party inspectors are invited to witness key stages: FEA review, weld documentation, and final load testing, ensuring transparency and quality assurance.

Case in Point: Eliminating Cracking at Feed Zone

The feed zone absorbs the highest impact forces. In a recent project for a copper mine, Haiside redesigned the feed box with a heavy-duty wear liner and a stress-relieved transition to the side plates. The previous screen had cracks developing within six months; the Haiside unit showed zero structural defects after two years of operation. This result underscores the importance of targeted reinforcement.

Conclusion: Invest in Long-Term Reliability

Avoiding structural failures in heavy-duty vibrating screens requires a holistic approach—from advanced FEA design and premium material selection to precision manufacturing and rigorous testing. While upfront costs may be higher, the total cost of ownership over a decade is significantly lower when unscheduled downtime and repairs are eliminated. Haiside’s engineering team works closely with clients to analyze specific operating conditions and tailor the screen structure accordingly. Choosing a partner with proven expertise in structural integrity is not just a purchase decision—it is an investment in operational continuity.

The Role of Vibrating Screens in Cement Production Quality Control

In cement manufacturing, consistent product quality is a non-negotiable requirement. Among the many process control tools, vibrating screens play an often-underestimated yet indispensable role in ensuring that raw materials, intermediate products, and final cement meet strict particle size specifications. A well-designed vibrating screen not only improves production efficiency but also directly impacts the uniformity of the finished product, reducing the risk of downstream defects. For plant managers and quality engineers exploring screening solutions, understanding how these machines contribute to quality control is the first step toward making an informed investment. This article examines the critical functions of vibrating screens in cement production, outlines the key parameters that influence screening performance, and presents the advantages of Haiside vibrating screens for achieving consistent quality outcomes.

Fundamental Role of Vibrating Screens in Cement Production

Vibrating screens are mechanical devices that separate bulk materials by particle size through vibration-induced stratification and passage. In cement production, they are deployed at multiple stages: from raw material crushing (limestone, clay, gypsum) to clinker cooling and final product finishing. Their primary quality control contributions include:

  • Consistent Raw Material Feed – By ensuring that raw materials entering the mill are within a specific size range, vibrating screens prevent oversized particles from damaging grinding equipment and maintain a uniform particle size distribution for optimal chemical reactions.
  • Intermediate Product Classification – After preheating and calcination, clinker must be cooled and screened to remove undersized or oversized fractions that could affect grinding efficiency. This step directly influences the Blaine fineness and compressive strength of the final cement.
  • Final Product Homogeneity – In the finishing mill circuit, vibrating screens classify the ground cement to achieve the desired particle size (typically <45 µm for Portland cement). Accurate screening ensures that the cement meets the required specific surface area and avoids quality rejects.

Each of these applications demands a screen that can handle high throughput, resist blinding (clogging), and deliver precise cut points under dusty, abrasive conditions. Without effective screening, variability in particle size leads to inconsistent setting times, reduced strength, and increased customer complaints.

How Vibrating Screen Design Affect Quality Control Performance

Cooperation Customer

Not all vibrating screens are equally effective in cement quality control. Several design and operational parameters determine whether a screen can maintain the required separation accuracy over time:

Vibration Mechanism and Amplitude Control

The vibration pattern (linear, circular, or elliptical) and amplitude directly affect material movement and stratification. For cement applications, linear motion screens are often preferred because they provide uniform acceleration across the entire deck, reducing the risk of particle segregation. Adjustable amplitude allows operators to fine-tune the screen for different materials without changing the eccentric mass. Haiside vibrating screens feature a robust eccentric shaft drive system that delivers consistent vibration energy even under varying feed loads, ensuring stable cut points.

Screen Media Selection

The type of screen deck – woven wire mesh, polyurethane panels, or rubber sheets – influences both durability and screening efficiency. In cement plants, wear and corrosion from moisture and fine particles accelerate media degradation. High‑tensile steel wire or polyurethane modular panels offer longer service life and resistance to blinding. Haiside offers a range of abrasion‑resistant screen media specifically engineered for cement environments, with open areas optimized to maximize throughput without compromising accuracy.

Anti‑Blinding Features

Blinding – when particles wedge into apertures or adhere to the screen surface – is a major cause of quality deviation. Vibrating screens for cement must incorporate features such as ball decks, ultrasonic vibrations, or trapezoidal wire to keep apertures clear. Haiside integrates an advanced self‑cleaning system that utilizes adjustable ball tray support to reduce blinding by up to 40% compared to conventional designs, maintaining consistent screening efficiency even with high‑moisture materials.

Key Factors in Choosing a Vibrating Screen for Cement Quality Control

When evaluating vibrating screen suppliers for a cement quality control application, decision‑makers should compare performance attributes that directly affect product consistency. The following table summarizes critical selection criteria and how Haiside screens address them:

Comparison of Screening Solutions for Cement Quality

  • Cut‑point accuracy: Standard screens may deviate ±2–3% from nominal aperture; Haiside screens achieve ±1% precision through precision‑manufactured decks and rigid frame construction.
  • Throughput capacity: Many screens lose separation efficiency at high loads. Haiside’s optimized vibration angle and adjustable stroke angle allow capacities up to 200 t/h on a single deck without sacrificing cut accuracy.
  • Durability in abrasive conditions: Haiside uses hardened steel side plates and replaceable wear liners in contact zones, extending service intervals by 30–50% compared to industry averages.
  • Ease of maintenance: Quick‑release deck panels and centralized lubrication points reduce downtime. Haiside screens are designed for fast media replacement – typically under 30 minutes per deck.
  • Automation & control integration: Haiside offers optional vibration frequency converters and real‑time amplitude monitoring, enabling automatic adjustments to maintain consistent separation despite feed variations.

Cement quality managers should also consider the supplier’s experience in the industry. Haiside has been supplying vibrating screens to cement plants for over 15 years, with a track record of helping clients achieve tighter quality specifications and lower rejection rates.

Conclusion

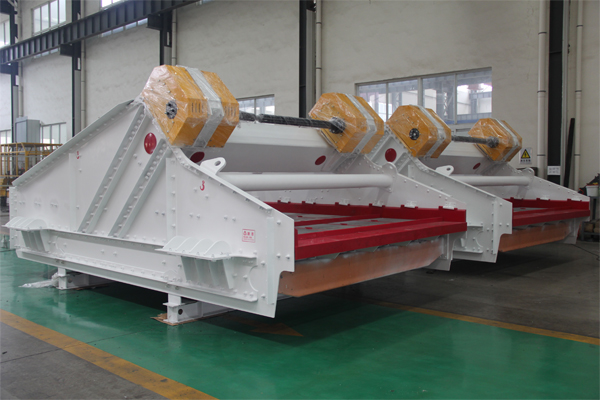
Single layer horizontal sieve

Vibrating screens are not auxiliary equipment but critical quality control components in cement production. From ensuring consistent raw material feed to achieving the precise fineness of finished cement, their performance directly impacts product uniformity, plant efficiency, and customer satisfaction. By selecting a screen with robust vibration control, anti‑blinding features, and durable construction – such as those offered by Haiside – cement manufacturers can reduce variability and maintain compliance with international standards. For organizations seeking to optimize their quality control process, a thorough evaluation of screening technology is an investment that pays dividends through lower rejects and higher operational reliability.

Multideck Vibrating Screens: Benefits for Separating Multiple Sizes

Multideck vibrating screens are engineered to simultaneously separate bulk materials into multiple particle size fractions, offering a significant efficiency advantage over single-deck configurations. For operators in mining, aggregates, recycling, and industrial processing, the ability to produce several product grades from a single machine reduces capital expenditure and floor space requirements. This article examines the core design principles, operational benefits, and application-specific advantages of multideck screens, with a focus on how Haiside’s robust engineering maximizes separation accuracy and throughput.

How Multideck Vibrating Screens Achieve Multi-Size Separation

A multideck vibrating screen typically consists of two, three, or four screen decks stacked vertically within a single vibrating frame. Each deck has a different mesh aperture, with the coarsest mesh on the top and progressively finer meshes below. Material enters the top deck, where vibration causes stratification: larger particles remain on top and are discharged as oversize, while smaller particles pass through to the next deck. This cascading action continues through each deck, producing up to four distinct size fractions (plus an undersize) in one pass.

Vibration Mechanism and Material Flow

The vibrating motion—typically circular, elliptical, or linear—is generated by one or two unbalanced motors or eccentric shafts. The amplitude, frequency, and angle of vibration are carefully tuned to maximize particle-bed fluidization and prevent blinding or pegging. Haiside screens feature adjustable vibration parameters, allowing operators to optimize performance for materials with varying moisture content, density, and particle shape.

Key Benefits of Multideck Screens for Multiple Size Separation

Compared to using multiple single-deck screens in series, a single multideck unit delivers several quantifiable advantages:

  • Reduced footprint and installation cost: One multideck machine replaces two to four single-deck screens, saving up to 50% of floor space and associated structural support.
  • Lower energy consumption: A single vibrating drive system powers all decks, reducing total power draw compared to multiple separate screens.
  • Higher overall throughput: Material is processed continuously across decks, with no need for intermediate conveyors or transfer points, minimizing bottlenecks and downtime.
  • Improved product quality: Sequential screening ensures each size fraction meets strict specifications, as overlarge particles cannot bypass fine decks. Haiside screens incorporate anti-blinding technologies such as ball trays and flexible rubber mats to maintain open area.
  • Simplified maintenance: Fewer bearings, belts, and motors mean less wear parts inventory and quicker service intervals. Haiside’s modular deck design allows rapid screen mesh changes without removing the entire cassette.

Critical Design Considerations for Reliable Operation

While multideck screens offer clear benefits, their performance depends on proper engineering. Key design parameters include:

  • Deck inclination: Steeper angles increase throughput but reduce accuracy; typical incline ranges from 15° to 25°. Haiside offers adjustable inclined models for flexible operation.
  • Mesh material and tensioning: Woven wire, polyurethane, or perforated plate options suit different abrasion levels. Proper tension prevents sagging that causes premature wear and inaccurate sizing.
  • Vibration isolation and structural integrity: Heavy-duty steel frames with rubber or spring mounts minimize transmitted vibration to the building or supporting structure.
  • Feed distribution: An even, well-dispersed feed is critical to avoid overloading one side of the top deck. Haiside integrates custom feed boxes and chute geometries to ensure uniform distribution.

Applications Across Key Industries

Cooperation Customer

Multideck vibrating screens are widely deployed in:

  • Aggregates and sand & gravel: Producing multiple product grades (e.g., 1/4”, 3/8”, 1/2”) from pit-run material, often paired with washing systems.
  • Mining and mineral processing: Classifying crushed ore before further comminution or separation processes. Three- and four-deck screens are common in iron ore, coal, and copper operations.
  • Recycling: Sorting construction and demolition debris, crushed concrete, or shredded scrap metal into usable fractions for resale or further processing.
  • Industrial powders: Fine screening of chemicals, fertilizers, or plastic pellets where precise particle size distribution is required.

Why Haiside Screens Are a Trusted Choice

Haiside has over a decade of experience designing and manufacturing multideck vibrating screens that withstand the harshest operating conditions. Our engineers apply finite element analysis to optimize screen box strength while minimizing weight. Every unit undergoes rigorous testing for vibration uniformity and noise levels before shipment. Haiside also provides customized solutions—such as dust covers, wear liners, and variable-frequency drive controllers—to match specific site requirements. With a global network of service representatives and readily available spare parts, Haiside ensures minimal downtime and maximum return on investment.

Conclusion: Multideck Efficiency for Modern Separation

Linear vibrating screen

Adopting a multideck vibrating screen is a proven strategy to boost classification accuracy, reduce equipment footprint, and lower operating costs. Whether you are expanding an existing plant or designing a new process line, careful selection of deck configuration, vibration parameters, and screen media will directly impact profitability. Partnering with an experienced manufacturer like Haiside ensures you receive a screen engineered for your specific material and throughput targets—delivering consistent, reliable multi-size separation for years to come.

Energy-Saving Technologies in Modern Vibrating Screen Designs

As industries such as mining, aggregates, and recycling face mounting pressure to reduce operational costs and meet sustainability goals, the vibrating screen—a critical piece of processing equipment—has become a focal point for energy efficiency improvements. Traditional vibrating screens often consume significant power due to inefficient drive mechanisms, suboptimal motion patterns, and outdated control systems. Modern designs, however, leverage advanced technologies that slash energy consumption without compromising screening performance. This article delves into the key energy-saving innovations reshaping vibrating screen design, and highlights how a leading manufacturer like Haiside is integrating these technologies to deliver tangible value to operators.

The Importance of Energy Efficiency in Vibrating Screen Operations

Vibrating screens are among the most energy-intensive machines in a processing plant, often operating 24/7. Even a modest reduction in power consumption can translate into thousands of dollars in annual savings per unit. Beyond direct cost benefits, energy-efficient designs reduce the carbon footprint of operations, aligning with global environmental regulations and corporate social responsibility targets. Moreover, efficient screens generate less heat, lowering maintenance requirements and extending component life. For these reasons, evaluating energy-saving features has become a critical factor in purchasing decisions for vibrating screens.

Key Energy-Saving Technologies in Modern Designs

Innovations in mechanical design, materials, and electronics have converged to create a new generation of energy-efficient vibrating screens. The following technologies are at the forefront:

High-Efficiency Vibrators and Drive Systems

Traditional screens rely on belt-driven exciters or unbalanced motors that waste energy through friction and transmission losses. Modern designs employ direct-drive vibrators with high-torque, low-current motors, often coupled with frequency inverters. These systems deliver the required centrifugal force at lower electrical loads. For instance, Haiside’s patented vibrator units use precision-balanced rotors and sealed bearings to minimize mechanical friction, achieving up to 15–20% lower energy consumption compared to conventional models.

Optimized Screen Deck Geometry

The angle and configuration of screen decks directly affect material flow and energy required to convey it. Modern screens feature adjustable inclination angles and curved deck profiles that enhance material stratification, allowing the same throughput at lower vibration amplitudes. Some designs incorporate polyurethane or rubber screen panels with reduced mass, which require less energy to oscillate while improving wear resistance. Haiside’s modular deck system, for example, enables operators to fine-tune the panel configuration based on feed characteristics, further optimizing energy use.

Advanced Control and Automation

Smart controllers with real-time load sensing and adaptive algorithms can automatically adjust vibration frequency and amplitude to match changing feed rates. This prevents over-screening—running at full power when the material load is light—and reduces energy waste. Additionally, modern screens integrate vibration monitoring sensors that detect imbalances or bearing wear early, allowing corrective action before inefficiency escalates. Haiside equips its screens with an intuitive control interface that displays real-time energy consumption per ton, enabling operators to make data-driven adjustments.

How Haiside Integrates Energy-Saving Technologies

Haiside stands out in the market by embedding energy efficiency into every aspect of its vibrating screen designs, from concept to aftermarket support. The company’s engineering team focuses on holistic optimization rather than merely adding energy-saving components. Below are the core strategies Haiside employs:

  • Custom-engineered vibrator selection based on the specific material density and screen size to avoid oversizing.
  • Finite element analysis (FEA) during the design phase to reduce structural weight without sacrificing rigidity, lowering the mass that must be vibrated.
  • Standard integration of variable frequency drives (VFDs) on all models above a certain size, allowing operators to match energy input to real-time demand.
  • Optional regenerative braking systems that capture and reuse energy during deceleration cycles in multi-deck or cascading screen setups.
  • Comprehensive training and commissioning to ensure the screen runs at its optimal operating point from day one.

Practical Benefits and ROI for Operators

Adopting energy-saving vibrating screen technology is not just an environmental gesture—it delivers measurable financial returns. Haiside’s customers have reported average energy savings of 18% in field trials, with some achieving over 25% in optimal conditions. These savings quickly offset the initial investment in premium components such as VFDs and high-efficiency motors. Additional benefits include reduced wear on screen panels due to lower vibration forces, extended bearing life, and decreased downtime for repairs. In one case study, a quarry replacing its legacy screens with Haiside’s energy-efficient models recouped the capital cost within 14 months through electricity savings alone.

Conclusion

Energy-saving technologies are no longer optional in modern vibrating screen design—they are a competitive necessity. From high-efficiency drives and optimized geometry to intelligent control systems, these innovations cut power consumption, lower operating costs, and support sustainable operations. Haiside has positioned itself as a leader in this space by integrating proven technologies into robust, field-tested designs. For plant operators seeking to upgrade their screening processes, evaluating the energy efficiency features of a vibrating screen should be a top priority. Choosing a partner like Haiside ensures that you not only receive cutting-edge technology but also the expertise to maximize its value throughout the equipment’s lifecycle.

Emergency Steps When Your Vibrating Screen Stops Running

A sudden stoppage of your vibrating screen can bring an entire production line to a halt, leading to costly downtime and potential material spillage. Whether you are a plant operator or maintenance manager, knowing the correct emergency steps to take is critical to minimize damage and restore operations safely. This guide outlines a systematic approach from immediate safety checks to professional repair considerations, with practical insights drawn from years of field experience. For complex repairs or replacement parts, Haiside offers specialized support to get your screen back online efficiently.

Immediate Safety and Diagnostic Steps

Before any troubleshooting, prioritize personal safety. A stopped vibrating screen may still hold electrical charge or have mechanically tensioned springs. Follow these actions in order.

1. Power Disconnection and Lockout

Turn off the main power supply to the screen and apply a lockout/tagout device to prevent accidental restart. Verify with a voltage tester that no current remains. Only then approach the equipment.

2. Visual Inspection

Look for obvious signs of trouble:

  • Burned or frayed wiring near the motor junction box
  • Foreign material jammed between screen decks or side plates
  • Broken springs or cracked support beams
  • Oil leaks from bearing housings
  • Overheated motor – touch with the back of your hand (after power off) to check for abnormal heat

3. Determine the Type of Stop

Was it a sudden stop with a loud bang? A gradual slowdown? Did the motor trip the circuit breaker? Each scenario points to different root causes. Record any alarms or error codes from the control panel before resetting.

Common Causes and Emergency Troubleshooting

Once safety checks are complete, diagnose the likely cause using the following hierarchy.

Motor and Electrical Issues

If the motor does not hum at all, check the starter, fuses, and thermal overload relays. A single-phase condition (one blown fuse) often causes the motor to hum but not rotate. In such cases:

  • Replace blown fuses with identical ratings.
  • Reset thermal overloads after they cool down (usually 5–10 minutes).
  • If the motor still fails, measure winding resistance with an ohmmeter – values more than 10% different between phases indicate a shorted winding, requiring motor replacement.

Important: Never restart the motor more than three times in quick succession; this can overheat and destroy the windings.

Mechanical Blockages or Bearing Failures

A jammed screen deck or failed bearing will cause excessive load and trip the motor. Rotate the eccentric shaft manually (use a bar if necessary) to feel for binding. If the shaft will not turn freely, you likely have:

  • A bearing seized up – disassemble and replace bearings; always use the correct grease type (typically lithium-based for vibrating screens).
  • Material packed under the screen mesh – remove the blockage carefully.

Vibration Mechanism Problems

If the motor runs but the screen does not vibrate properly, the coupling between motor and exciter may be broken, or the exciter weights may have loosened. Check for:

  • Sheared rubber bushings or universal joints
  • Loose bolts on vibrating body (can cause imbalance and sudden stop)
  • Broken springs – replace in matched sets to maintain stroke uniformity

When to Call for Professional Repair or Replacement

Not all stoppages can be resolved on-site. The table below helps you decide whether to proceed with internal resources or contact Haiside for expert service.

DIY vs Professional Repair Criteria
Situation Recommended Action Why
Blown fuse or tripped overload (no visible damage) Replace/reset, monitor Low risk, common occurrence
Foreign material jam Clear blockage manually Simple if safe access
Shaft won’t turn / bearing damage Call Haiside service Precision fitting and alignment required; incorrect bearing replacement can cause catastrophic failure
Motor winding shorted Replace motor (or rewind by specialist), consult Haiside for correct specification Incorrect motor mounting or power rating leads to repeat failure
Structural crack on side plate Stop immediately, call engineer Weld repair must comply with stress-relief procedures; Haiside can supply reinforcement kits
Repeated stops without clear cause Full inspection by Haiside technician Potential resonance, weakening structure, or electrical system issues

Preventive Maintenance Tips to Avoid Future Stoppages

Emergency steps are only half the battle. A proactive maintenance program dramatically reduces unexpected downtimes. Implement the following based on manufacturer guidelines (Haiside recommends monthly checks for heavy-duty screens):

  • Daily: Listen for unusual noise; check belt tension and vibration amplitude.
  • Weekly: Grease bearings per schedule; inspect screen mesh for wear or holes.
  • Monthly: Torque all bolts on exciter, motor base, and spring mounts to specified values.
  • Quarterly: Replace worn springs; measure motor current to detect imbalance.
  • Annually: Overhaul bearings and inspect side plate integrity; consider Haiside’s comprehensive service package.

Record keeping is essential. Log all emergency stops and repairs – patterns (e.g., same bearing failing every 6 months) indicate a systemic issue such as incorrect lubrication or misalignment.

Conclusion

When your vibrating screen stops running, a calm, methodical response saves time and prevents further damage. Start with safety lockout, visually inspect, then isolate the cause using the diagnostic steps above. For electrical faults, simple fuse replacements can be handled in-house; mechanical failures like bearing or shaft damage warrant professional intervention. Haiside’s experienced engineers can provide on-site diagnosis, genuine replacement parts, and even screen upgrades to improve reliability. By combining emergency preparedness with regular preventive maintenance, you ensure that your screening process remains efficient and productive.

For immediate assistance or to schedule a maintenance audit, contact Haiside – your partner in vibrating screen reliability.

QA and QC Tests Every Vibrating Screen Operator Should Know

Every vibrating screen operator knows that consistent screening performance depends on more than just starting the machine and feeding material. Quality Assurance (QA) and Quality Control (QC) tests form the backbone of reliable operation, helping to detect wear, misalignment, and process deviations before they lead to costly downtime or product quality failures. Whether you are new to screening operations or a seasoned professional, mastering these fundamental tests ensures your equipment delivers the expected gradation, throughput, and longevity. In this guide, we outline the core QA and QC tests that every operator should integrate into their routine, drawing on industry best practices and the engineering expertise of Haiside.

1. Pre-Operational Inspection: The Foundation of QA

Before any load is applied, a thorough pre-operational check verifies that the vibrating screen is mechanically sound and safe to start. This QA step establishes a baseline for all subsequent tests.

1.1 Visual and Structural Examination

Inspect the screen deck, side plates, cross beams, and support structure for cracks, deformation, or loose bolts. Particular attention should be paid to weld joints and areas around the exciter mounting. Haiside recommends using a calibrated torque wrench to verify that all fasteners meet the manufacturer’s specified torque values.

1.2 Vibration Mechanism Check

Ensure the exciter (vibrator) is correctly assembled with the proper oil level and no leaks. Rotate the exciter manually (if possible) to confirm free rotation without binding. Check that the drive belts or coupling are aligned and tensioned per specifications.

1.3 Safety Systems Verification

Test emergency stops, interlocks, and guards. Confirm that the screen is isolated from upstream and downstream equipment before start-up.

2. Dynamic Performance Tests: Amplitude, Frequency, and Stroke

Once the screen is running at no-load, operators must measure key vibration parameters to confirm the machine is operating within design tolerances.

2.1 Amplitude Measurement

Amplitude (travel) is the total displacement of the screen deck. Use a vibration analyzer or a simple amplitude measurement card to record the peak-to-peak displacement at all four corners of the deck. The acceptable variation between corners should be less than 10%. Haiside engineers emphasize that amplitude below specification reduces stratification efficiency, while excessive amplitude accelerates structural fatigue.

2.2 Operating Frequency (RPM)

Using a tachometer or built-in encoder, verify that the exciter speed matches the manufacturer’s target frequency. Any deviation of more than 5% may indicate belt slippage, electrical frequency issues, or incorrect pulley ratios.

2.3 Stroke Angle and Direction

On linear motion screens, confirm the stroke angle (typically 30–45 degrees) using an inclinometer or by observing the attached angle indicator. Erroneous stroke angles lead to poor material travel and inefficient screening.

3. Screening Media Integrity and Tension QC

The condition and tension of the screen cloth or polyurethane panels directly influence cut-point accuracy and blinding.

3.1 Visual Mesh Inspection

Examine each panel for broken wires, worn apertures, and tears. For woven wire cloth, use a magnifier to check for fatigue cracks at the crimp points. Replace any panel where more than 5% of the apertures are enlarged beyond the allowed tolerance.

3.2 Tension Verification

Proper tension prevents sagging and premature failure. Use a tension meter to measure the force applied to the screen cloth. Haiside recommends a tension of 900–1100 N/cm for typical woven wire applications. Re-tension after the first 24 hours of operation and then weekly.

3.3 Seal and Gasket Check

Inspect the edge seals and gaskets between deck modules. Gaps permit bypass (fines leaking around the screen cloth), which is a common QC failure that can go unnoticed for hours.

4. Loaded Testing and Process Validation

QA is not complete until the screen is tested under actual material feed conditions.

4.1 Material Bed Depth and Velocity

Using a scale marker on the feed box, observe the depth of the material bed across the entire width of the screen. Ideal bed depth should not exceed 4–5 times the aperture size for efficient stratification. Measure material travel velocity (ft/min) by tracking a marked stone; compare to the expected value.

4.2 Screening Efficiency Calculation

Collect samples of feed, oversize, and undersize streams. Perform a sieve analysis to determine the actual efficiency (percentage of material smaller than aperture that passes through). Efficiency values below 85% often indicate worn media, incorrect amplitude, or feed distribution issues.

4.3 Deck Loading and Balanced Flow

Check that material is evenly distributed across all decks. Uneven loading leads to localized blinding and accelerated wear. If necessary, adjust the feed chute or diverter.

5. Predictive Maintenance: Oil Analysis and Vibration Trends

For advanced operators, QC extends beyond daily checks into trend monitoring.

5.1 Exciter Oil Analysis

Send periodic oil samples to a lab for wear metal analysis. Rising levels of iron, copper, or silicon indicate bearing or gear wear before catastrophic failure. Haiside suggests quarterly sampling for screens operating more than 12 hours per day.

5.2 Vibration Spectrum Trending

Use an FFT vibration analyzer to capture baseline signatures. Changes in the 1× or 2× running speed amplitudes can signal imbalance, bearing degradation, or structural looseness. Store weekly readings and compare to the baseline.

FAQ – Common Questions from Vibrating Screen Operators

  1. How often should I perform amplitude checks? At least daily during the first week of operation, then weekly once stable. Always after replacing exciter components or screen media.
  2. What is the fastest way to detect screen cloth blinding? Observe the flow pattern on the deck: if material accumulates in one area or the oversize stream appears wet, blinding is likely.
  3. Can I use the same QC procedures for banana screens and circular motion screens? The principles are the same, but the stroke angle and measuring points differ. Always refer to the specific equipment manual provided by Haiside or your OEM.
  4. What should I do if screening efficiency drops by 10% without visible damage? First, re-check amplitude and feed rate. Next, verify that the screen slope is correct. Finally, perform a distribution test to rule out feed segregation.

Conclusion

QA and QC tests are not bureaucratic overhead; they are the operator’s primary tools to ensure consistent product quality, maximize throughput, and extend equipment life. By systematically performing visual inspections, vibration measurements, media checks, and process validation, operators can catch small issues before they escalate into major failures. Haiside provides detailed test protocols and training for every screen model, empowering operators to maintain peak performance day after day. Start your next shift with a structured test checklist—your screen and your customers will thank you.